
 English
 日本語
 Deutsch
Industry News
 Oct 01, 2026
 Posted by Administrator
Why Aluminum Housings Decide Whether Your Automotive Sensor Survives the Road
Why a Sensor Housing Is an Engineering Decision, Not a Packaging Detail
A camera module that drifts two pixels out of alignment, a radar unit that overheats on a summer highway, a LiDAR enclosure that fogs after a pressure wash: these are not sensor failures. They are housing failures. By the time a vehicle platform reaches validation, the enclosure has already fixed the thermal path, the optical datum, the seal integrity, and the corrosion budget for the next fifteen years.
Modern vehicles carry a growing population of sensors. Camera, radar, LiDAR, ultrasonic, and environmental sensing units each impose different demands on the housing that protects them. An optical sensor cares about flatness and parallelism. A radar module cares about dimensional stability across temperature. A LiDAR unit cares about heat extraction from a small, hot package. All of them care about moisture, dust, salt, and vibration.
Aluminum has become the default answer for most of these enclosures, and for good reason. It offers a strength-to-weight ratio that steel cannot match, thermal conductivity in the 200 to 230 W/m·K range, natural corrosion resistance through its passive oxide layer, and full compatibility with anodizing, powder coating, and laser welding. The interesting engineering work is not in choosing aluminum. It is in choosing which aluminum, produced which way, held to which tolerances.
This guide works through six selection factors in the order they tend to surface in a real program: material, tolerance and fit, thermal management, ingress protection, surface treatment, and supply chain. Each section includes the questions worth asking a manufacturing partner before tooling is cut.
The core trade-off
Every housing decision trades mass against stiffness, tolerance against cost, and thermal performance against manufacturability. There is no universally correct specification, only a specification that matches the sensor's failure modes.
Factor 1: Material Selection Across the Aluminum Alloy Spectrum
The alloy determines strength, thermal conductivity, corrosion behavior, weldability, and how well the surface will anodize. A wrong choice shows up later as stripped threads, a hot spot that never dissipates, or a finish that mottles after coating.
| Alloy | Typical Property Profile | Best Fit for Sensor Housings |
|---|---|---|
| Al1070 | High purity, very high thermal conductivity, excellent laser weldability | Hermetically sealed housings, thermal-critical modules |
| 6061 | Good strength, excellent corrosion resistance, weldable | Structural housings, mounting brackets |
| 6063 | Excellent extrudability, smooth as-formed surface | Complex profiles, integrated heat sink bodies |
| 7075 | Very high strength, fatigue resistant | High-load and vibration-critical mounts |
How to Narrow the Choice
- Operating temperature range and peak heat load
- Mechanical load path and fastener requirements
- Sealing method, especially whether laser welding is planned
- Surface finish and coating requirements
- Availability in the required extrusion or forging form
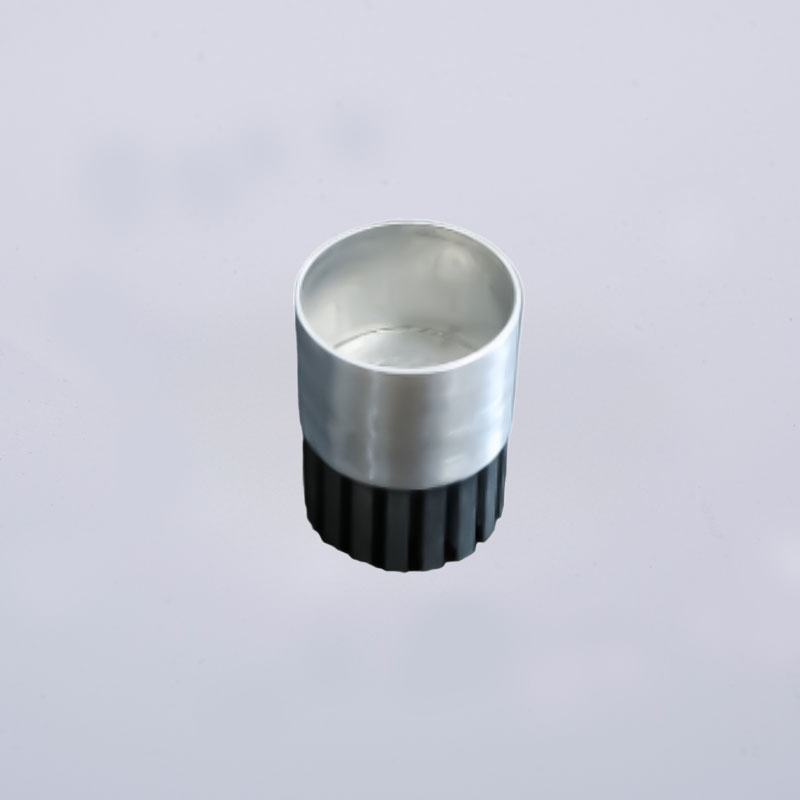
For thermal-critical and hermetically sealed sensor packages, high-purity alloys such as Al1070 are frequently specified because they combine heat spreading with reliable laser welding. For structural brackets that also act as heat sinks, 6061 or 6063 usually gives a better balance of cost and machinability. Vibration-heavy mounting points push toward 7075.
Factor 2: Dimensional Tolerance and Fit
A sensor housing performs two precision jobs at once. It locates optical or electromagnetic components relative to each other, and it closes a seal against the environment. Both jobs are tolerance problems.
| Feature Class | Typical Requirement | Process That Delivers It |
|---|---|---|
| General dimensions | plus or minus 0.1 mm | Cold extrusion or die casting |
| Critical features | plus or minus 0.02 mm | CNC finishing after forming |
| Optical mounting surfaces | Flatness and parallelism in the micron range | Precision CNC with CMM verification |
Why the Forming Process Sets the Ceiling
Cold extrusion produces near-net shapes with good dimensional accuracy and a dense grain structure. CNC machining then brings critical features into final tolerance without disturbing the overall geometry. The combination is what allows a housing to be structurally sound and optically precise at the same time.
Verification Is Part of the Specification
- Coordinate measuring machine inspection for datum and position
- Optical comparators for profile checks
- Surface profilometry for flatness and roughness
- Documented inspection records for PPM stability
Practical rule
Specify tight tolerances only where the sensor actually needs them. Every micron of extra precision adds machining time, and machining time is the most controllable cost lever in the program.
Factor 3: Heat Dissipation and Thermal Management
Camera, radar, and LiDAR modules generate heat continuously during operation. Temperature rise degrades accuracy, accelerates component aging, and introduces thermal drift that no calibration routine can fully compensate. The housing is the primary heat exchanger.
Thermal Design Principles
- Maximize exterior surface area for convection
- Keep an uninterrupted heat path from source to outer wall
- Avoid internal porosity, which acts as a thermal barrier
- Match fin geometry and orientation to airflow direction
- Choose surface treatments that do not insulate the housing
Process Impact on Thermal Performance
Cold extrusion produces a dense, essentially pore-free structure. Because heat must travel through solid metal, eliminating porosity preserves an uninterrupted thermal path. In comparative testing, cold extruded aluminum housings have demonstrated thermal performance up to 2.36 times better than equivalent die cast housings, largely because die casting introduces gas porosity that interrupts conduction.
| Design Feature | Thermal Benefit |
|---|---|
| Integrated heat sink fins | Increases convective surface area |
| Thermal pads or gap fillers | Closes air gaps between component and wall |
| Chassis mounting surface | Provides a secondary conduction path |
| Thin, conductive coatings | Preserves heat transfer at the surface |
Factor 4: Ingress Protection and Sealing Strategy
An exterior sensor sees rain, road spray, dust, salt, and repeated temperature cycling. Ingress protection is what keeps the interior dry and clean over the vehicle lifetime.
| Rating | Protection Level | Typical Sensor Position |
|---|---|---|
| IP67 | Dust-tight, protected against temporary immersion | Body-mounted radar and camera units |
| IP68 | Dust-tight, protected against continuous immersion | Low-mounted or exposed modules |
| IP69K | Protected against high-pressure, high-temperature washdown | Commercial vehicle and off-highway sensors |
Sealing Methods and Their Housing Requirements
- O-ring grooves: require precise groove dimensions and smooth sealing faces
- Gasket channels: need consistent channel depth and surface finish
- Laser welding: requires a weldable, high-purity alloy and clean mating surfaces
- Ultrasonic welding: depends on controlled energy directors and material consistency
- Adhesive bonding: sensitive to surface contamination and roughness
Pressure tightness starts with the material. A pore-free structure has no leak path to begin with, which is why cold extrusion is often specified for sealed sensor housings. Ultrasonic cleaning before sealing or bonding removes oils and particles that would otherwise create a channel or a weak bond line.
Sealing insight
Most field leaks trace back to the interface, not the bulk material. Groove geometry, surface roughness, and cleanliness deserve as much attention as the alloy specification.
Factor 5: Surface Treatment and Corrosion Resistance
Exterior housings face salt spray, road chemicals, ultraviolet exposure, and thermal cycling. Surface treatment provides corrosion resistance, wear resistance, and the appearance quality that visible sensor modules now require.
| Treatment | Characteristics | When to Specify |
|---|---|---|
| Anodizing | Thick hard oxide layer, excellent corrosion resistance, color options | Exterior housings needing durability and appearance |
| Powder coating | Durable thick finish, wide color range, good corrosion protection | Visible covers and brackets |
| Conversion coating | Thin, conductive, good for grounding | Interfaces requiring electrical continuity |
| Laser marking | Permanent identification and traceability | Part numbering and lot tracking |
Selection Criteria
- Environmental exposure severity and expected service life
- Appearance and color requirements
- Need for electrical conductivity or insulation
- Cost and process availability
Surface finish before coating matters more than most teams expect. Lower roughness improves coating adhesion and produces a more uniform final appearance. Cold extrusion delivers an excellent as-formed surface, which reduces the preparation work needed before anodizing or powder coating.
Factor 6: Lead Time, Capacity, and Supply Chain Reliability
Automotive development cycles are compressed. A housing that arrives late delays validation, PPAP, and start of production, regardless of how well it is made.
Where Lead Time Actually Goes
- Tooling design and fabrication
- First article sampling and approval
- Production scheduling and material procurement
- Surface treatment queue
- Inspection, packaging, and shipping
Capacity Questions Worth Asking
- How many extrusion lines are available, and across what tonnage range
- What is the annual unit capacity
- Is CNC machining performed in house
- Are anodizing and powder coating performed in house
- Can the supplier scale from prototype to mass production without requalification
Vertical integration is the strongest predictor of schedule reliability. When extrusion, cold extrusion, CNC machining, and surface treatment sit under one roof, handoffs disappear, quality feedback loops shorten, and the schedule stops depending on third-party queues. Long-term partnerships for plastic and stainless steel accessories further simplify sourcing for a complete sensor assembly.
Supply chain insight
Ask for capacity numbers, not capacity claims. Annual unit output, line count, and tonnage range are verifiable. General statements about being a full-service manufacturer are not.
Selection Checklist for Custom Aluminum Sensor Housings
| Factor | Question to Ask | What Good Looks Like |
|---|---|---|
| Material | Which alloy balances thermal, mechanical, and corrosion needs? | High-purity alloy for thermal and welding, 6061 or 6063 for structural |
| Tolerance | What tolerances do optical alignment and sealing require? | 0.1 mm general, 0.02 mm on critical features |
| Thermal | What is the heat load and required thermal path? | Dense, pore-free wall with integrated fins |
| IP Rating | Which rating and sealing method apply? | Pore-free material, clean interfaces, validated weld or seal |
| Surface | What exposure and appearance are required? | Anodizing or powder coating matched to environment |
| Lead Time | What is the timeline from design freeze to SOP? | Integrated extrusion, CNC, and finishing capacity |
| Quality | What PPM target and documentation are required? | Documented inspection, CMM data, consistent PPM |
Aluminum Cold Extrusion vs Die Casting for Sensor Housings
This comparison comes up in nearly every sensor housing program, and the answer depends on which failure mode matters most.
| Attribute | Cold Extrusion | Die Casting |
|---|---|---|
| Internal porosity | Essentially pore-free | Gas porosity is common |
| Thermal path | Uninterrupted, up to 2.36 times better in comparative tests | Interrupted by pores and inclusions |
| Pressure tightness | Excellent, no leak paths | Requires impregnation or sealing in some cases |
| Dimensional accuracy | Good as-formed, excellent after CNC | Good for complex geometry |
| Best fit | Sealed, thermal-critical sensor housings | Complex thin-wall geometries with lower thermal demand |
Where a sensor must be hermetically sealed or must shed significant heat, cold extrusion has a structural advantage that no downstream process can fully recover. Where geometry complexity dominates and thermal load is modest, die casting remains competitive.
Frequently Asked Questions
Q1: Which aluminum alloy is best for an automotive sensor housing?
There is no single best alloy. High-purity alloys such as Al1070 suit thermal-critical and laser-welded housings. 6061 and 6063 suit structural housings and complex extruded profiles. 7075 suits high-load or vibration-critical mounts. The correct choice follows from operating temperature, mechanical load, sealing method, and surface finish requirements.
Q2: What tolerance can realistically be achieved on a sensor housing?
General dimensions typically hold to about 0.1 mm after cold extrusion or die casting. Critical features can reach about 0.02 mm with CNC finishing. Optical mounting surfaces often require flatness and parallelism in the micron range, verified by CMM inspection.
Q3: Why does cold extrusion outperform die casting thermally?
Die casting introduces gas porosity into the metal. Porosity interrupts the conduction path and creates local hot spots. Cold extrusion produces a dense, essentially pore-free structure, so heat travels through solid metal. Comparative testing has shown up to 2.36 times better thermal performance for cold extruded housings.
Q4: What IP rating should an exterior automotive sensor housing target?
IP67 is common for body-mounted radar and camera units. IP68 applies to low-mounted or continuously exposed modules. IP69K is specified where high-pressure, high-temperature washdown occurs, such as commercial vehicle and off-highway applications.
Q5: Does surface treatment affect heat dissipation?
Yes. Thick insulating coatings add thermal resistance at the surface. Anodizing and conversion coatings are generally thin enough to preserve heat transfer, while heavy powder coating builds should be evaluated against the thermal budget.
Q6: How can lead time be reduced for a new sensor housing program?
Choose a supplier with integrated extrusion, cold extrusion, CNC machining, and surface treatment. In-house process control removes third-party queues, shortens the sampling loop, and reduces the risk of schedule slippage between process steps.
Q7: What should be included in a request for quotation?
Provide 3D models and 2D drawings with datum strategy, alloy preference or performance requirements, sealing method, IP rating target, surface treatment specification, annual volume, and required delivery milestones. DFM feedback at quotation stage often prevents tooling changes later.
Specifying the Right Housing Starts With the Right Questions
A sensor housing is a thermal device, a precision fixture, a seal, and a corrosion barrier at the same time. Each of the six factors above can become the limiting one depending on the application. The teams that get this right tend to be the ones that define the failure modes first, then specify material, tolerance, thermal design, sealing, finish, and supply chain against those failure modes.
When evaluating a manufacturing partner, look for integrated process capability rather than a catalogue. Extrusion, cold extrusion, CNC machining, ultrasonic cleaning, surface treatment, and full inspection under one roof is what turns a specification into a repeatable part. The same integration is what makes aluminum cold extrusion parts viable for sealed and thermal-critical sensor enclosures at production volume.
Send drawings and performance requirements early. DFM feedback at the quotation stage is far cheaper than a tooling change after first article.
-
Tel Number
+86-0572-2210226Phone Number
+86-13819283977 +86-13655726561 +86-13567228000Address
Building B, Innovation and Entrepreneurship Industrial Park, No. 288, Yansan Road, Huzhou City, Zhejiang Province, ChinaQrCode
-
Quick Links
Home Products About Us Capabilities Industries News Contact Us -
Explore
Aluminum Camera Shell Of Vehicle Aluminium Cold Extrusion Aluminium Cold Forging Parts -
feel free to contact us